 SolarCalculators
Cement Plant Waste Heat Recovery (WHRS) + Rooftop Solar Hybridization 2026
1. The Power Architecture of a Modern Cement Plant
Electrical power in an integrated dry-process cement plant is split across distinct operational areas:
| Cement Process Area | Power Demand Nature | Connected Electrical Load | Captive Energy Supply Matching |
|---|---|---|---|
| Raw Material Grinding (VRM / Ball Mills) | Continuous heavy motor grinding | 15 MW to 25 MW | Supplied by continuous baseload WHRS generation |
| Rotary Kiln & Preheater Fan Drives | 24x7 mission-critical high-inertia fans | 8 MW to 14 MW | Dedicated captive power with zero allowable blinks |
| Cement Mills & Packaging Plants | Heavy daytime grinding and automated packing/dispatch | 10 MW to 20 MW (Peaks during daytime dispatch hours) | 100% Daylight Match for Rooftop Solar PV Generation |
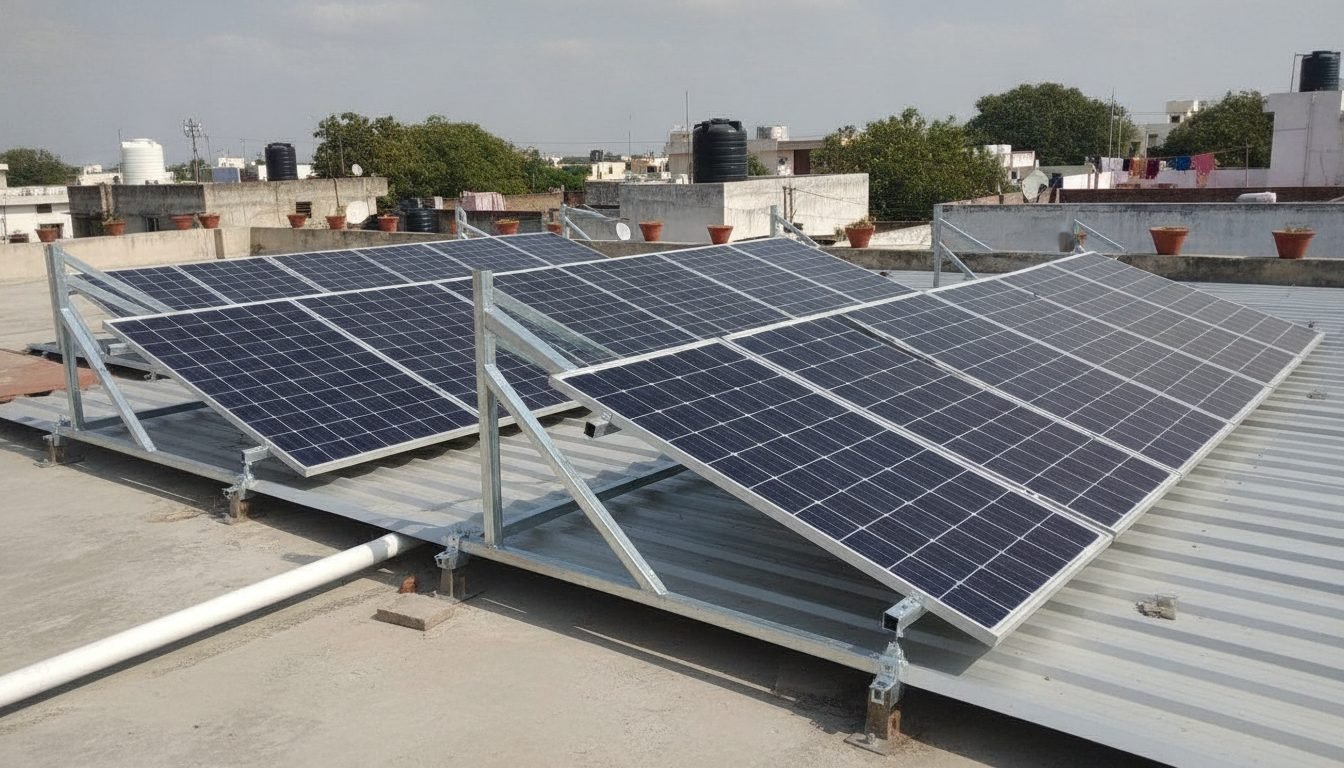
| Limestone & Clinker Covered Storage Sheds | Massive expansive arch-barrel roofs (1,00,000+ sq.ft.) | Zero internal power draw | Ideal footprint for 3 MW to 10 MW Rooftop Solar Arrays |
2. The Cement Clinker Dust Challenge: Alkalinity & Anti-Etch Glass
Installing solar panels inside a cement manufacturing perimeter presents an aggressive chemical environment unlike any standard industrial setting:
- Extreme Alkalinity (pH 11 to 13): Cement kiln dust (CKD) contains high concentrations of calcium oxide (\(\text{CaO}\)), potassium, and sodium. When combined with morning dew or monsoonal rain, it forms highly alkaline calcium hydroxide (\(\text{Ca(OH)}_2\)).
- Chemical Glass Etching: Alkaline solutions attack standard silica module glass, leaching silicates and causing irreversible milky white glass etching within 18 months unless protected.
- Anti-Etch Hydrophobic Coatings: Modules deployed in cement plants must feature factory-cured hydrophobic and oleophobic fluoropolymer nano-coatings that prevent alkaline dust from reacting with the underlying glass substrate.
- Vibration-Isolated Rail Mountings: Clinker conveyor galleries and vibrating screening sheds generate continuous low-frequency mechanical vibrations (\(10\,\text{Hz} - 50\,\text{Hz}\)). Module mounting structures must deploy EPDM vibration-damping isolators and locking wedge washers to prevent structural bolt fatigue.
3. Dispatch Economics: Solar PV + WHRS Synergistic Dispatch
The operational hybridization of Waste Heat Recovery and Solar PV operates with perfect thermodynamic and economic synergy:
Baseload WHRS (Steam Turbine): Preheater exhaust (300°C–350°C) and cooler exhaust (250°C–300°C) produce superheated steam driving a steam turbine generator (STG), delivering 10 MW to 15 MW of continuous round-the-clock power @ ₹1.40/kWh O&M cost.
Daytime Solar PV Peak Shaving: During afternoon peak production hours when raw mills, cement mills, and dispatch lines run simultaneously, the 10 MW Rooftop Solar array injects peak green power, completely displacing expensive grid power (commercial tariff ₹7.80–₹9.20/kWh).
Blended Captive Cost of Energy: Combining 65% WHRS generation + 35% Solar PV generation delivers a blended industrial captive power cost of ₹2.85 to ₹3.15 per unit, saving an integrated cement plant over ₹20 to ₹35 Crores annually in operating power expenses.
4. Structural Modeling on Expansive Clinker Dome Roofs
Covered limestone and clinker storage sheds feature vast curved space-frame arches spanning 60 to 90 meters without central columns. Engineering solar PV on these structures requires specialized civil checks:
- Curvature Wind Uplift Analysis: Airflow acceleration over curved barrel vaults creates high localized suction at the crown. Wind tunnel modeling under IS 875 (Part 3) mandates heavy-duty aluminium standing-seam clamps with pull-out strengths exceeding 3.2 kN per attachment point.
- Dead Load Safety Margin: The added dead load of solar modules and framing (12–14 kg/m²) represents less than 8% of the space frame's structural design capacity, easily verified through STAAD.Pro 3D space-frame simulation.